Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | CHINA |
| Brand Name: | YUHONG |
| Certification: | ABS, GL, DNV, NK, PED, AD2000, GOST9941-81, CCS, ISO 9001-2008 |
| Model Number: | S31803, S32750, S32760, SUS329J3L, 1.4462, 1.4410, 1.4501 |
| Minimum Order Quantity: | 100KGS |
|---|---|
| Packaging Details: | PLYWOOD CASE,BUNDLE |
| Delivery Time: | 7DAYS |
| Payment Terms: | L/C,T/T |
| Standard: | ASTM A789 / ASTM A790 / ASTM A928 | Material: | S31803, S32750, S32760, SUS329J3L, 1.4462, 1.4410, 1.4501 |
|---|---|---|---|
| NDT: | ET,UT,PT,HT | END: | PLAIN,BEVELED |
| TYPE: | SEAMLESS,WELDED | Brand: | CHINA |
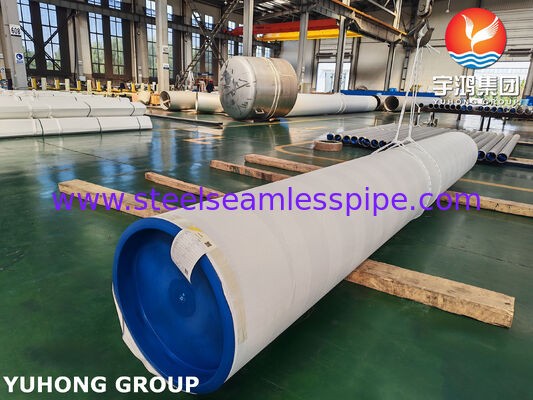
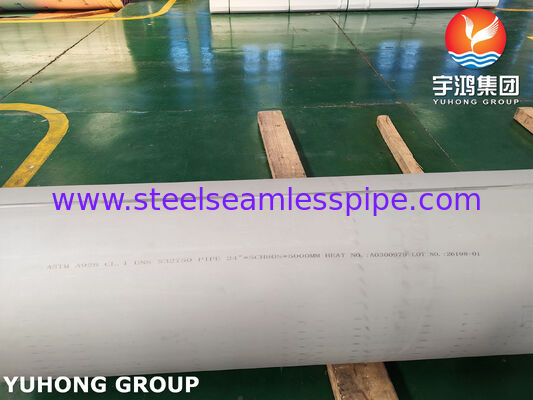
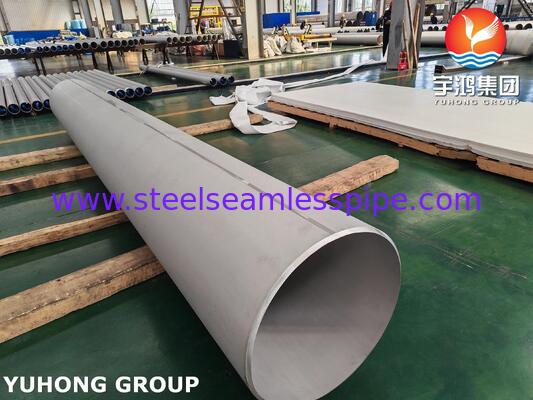
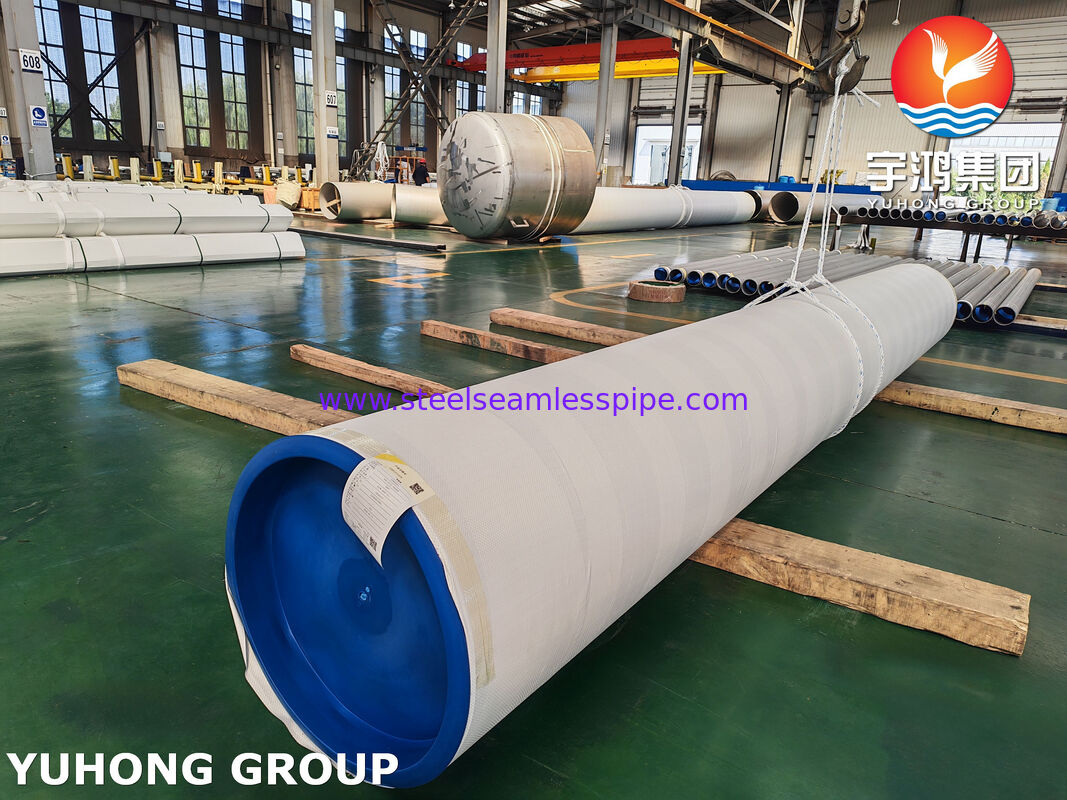
ASTM A928 CL.1 UNS S32750 Welded Pipe SAF 2507 / EN 1.4410 Electric Fusion Welded, 100% RT Super Duplex Pipe
YUHONG GROUP deal with stainless steel seamless pipe and tube already more than 10 years, every year sell more than 80000 tons of stainless steel seamless pipe and tube. Our client already cover more than 45 countries. Our stainless steel seamless pipe and tube was width used in Mining, Energy, Petrochemical, Chemical Industry, Food plant, Paper plant, Gas and Fluid Industry etc.
| Field | Value |
|---|---|
| Product Name | ASTM A928 CL.1 UNS S32750 Super Duplex Stainless Steel EFW Pipe |
| Product Type | Electric Fusion Welded (EFW) pipe, longitudinal seam |
| Specification Standard | ASTM A928/A928M Class 1 (also ASME SA-928) |
| Class Definition | Double welded with filler metal in all passes + 100% full radiographic examination |
| Material (Grade) | UNS S32750 Super Duplex Stainless Steel (25Cr–7Ni–4Mo–N) |
| Material Equivalents | EN 1.4410 / X2CrNiMoN25-7-4 / SAF 2507 / ASTM A182 F53 |
| PREN | ≥ 40 (typical ≈ 42) |
| Outside Diameter | 1/2" – 24" (DN15 – DN600), others on request |
| Wall Thickness | SCH 5S – SCH XXS, custom wall available |
| Length | Random length / 6 m / 12 m / cut-to-length |
| End Finish | Beveled to ASME B16.25, plain end on request |
| Surface | Annealed & pickled; blasted optional |
| Heat Treatment | Solution annealed 1050–1125 °C, rapid cooling |
| MOQ | 1 ton (trial / sample order negotiable) |
| Lead Time | 30–45 days after PO confirmation and drawing approval |
| Certification | EN 10204 3.1 mill certificate; 3.2 third-party inspection optional |
| Packing | Wooden crate / bundled with end caps, sea-worthy export packing |
| Payment Terms | T/T 30% deposit + 70% before shipment, or L/C at sight |
| Document / Code | Scope |
|---|---|
| ASTM A928/A928M Class 1 | EFW duplex stainless steel pipe with filler metal; double welded in all passes, completely radiographed |
| ASME SA-928 | ASME pressure-vessel / pressure-piping equivalent of A928 |
| ASTM A790 | Counterpart seamless & welded super duplex pipe spec; S32750 grade requirements referenced |
| ASME B36.10M / B36.19M | Pipe dimensions, wall schedules and weights |
| ASME B16.25 | Buttwelding end (bevel) preparation |
| ASTM A370 / E1019 | Mechanical test methods and chemical analysis methods |
| ASTM G48 | Pitting and crevice corrosion resistance test |
| ASTM A262 | Intergranular corrosion susceptibility test |
| EN 10204 3.1 / 3.2 | Material certification type |
| NACE MR0175 / ISO 15156 | Sour (H₂S) service suitability, where specified |
| ASME B31.3 | Process piping design basis for allowable stress and temperature limits |
Documentation delivered
Testing evidence
| Element | Min | Max |
|---|---|---|
| C | — | 0.030 |
| Si | — | 0.80 |
| Mn | — | 1.20 |
| P | — | 0.035 |
| S | — | 0.020 |
| Cr | 24.00 | 26.00 |
| Ni | 6.00 | 8.00 |
| Mo | 3.00 | 5.00 |
| N | 0.24 | 0.32 |
| Cu | — | 0.50 |
| Fe | Balance | — |
| Property | Value | Remark |
|---|---|---|
| Tensile strength, Rm | ≥ 795 MPa (115 ksi) | A928 / A790 requirement |
| Yield strength, Rp0.2 | ≥ 550 MPa (80 ksi) | ≈ 2× 316L |
| Elongation, A | ≥ 25% | Standard specimen |
| Hardness | ≤ 300 HB | Finished pipe |
| Ferrite content | 35–55% | Balanced duplex structure |
| PREN | ≥ 40 (typ. ≈ 42) | Cr + 3.3Mo + 16N |
| Heat treatment | 1050–1125 °C solution anneal + rapid cool | Mandatory after welding |
| Density | 7.8 g/cm³ | — |
| Thermal expansion | 13.0 × 10⁻⁶ /K (20–100 °C) | Lower than austenitics |
| Thermal conductivity | ≈ 14 W/m·K | Higher than austenitics |
| Parameter | Range / Limit |
|---|---|
| Service temperature | −40 °C to +250 °C continuous |
| Upper limitation | Avoid prolonged exposure above ~300 °C (sigma-phase precipitation); 475 °C embrittlement zone must be avoided. Design allowable stress per ASME B31.3. |
| Corrosive environment | Seawater, chloride brines, process acids, humid salt atmosphere. Pitting/crevice resistance supported by PREN ≥ 40. |
| Sour service (H₂S) | Only where qualified to NACE MR0175 / ISO 15156. |
| Max chloride level | Suitable for high-chloride service; verify specific concentration/temperature combination against the corrosion curve. |
| Welding (field) | GTAW / SMAW with ER2594 / E2594 filler; no preheat; interpass ≤ 150 °C; no PWHT required. |
Note: MOQ, lead time and dimensional ranges above are reference commercial terms, subject to final PO confirmation. Chemical and mechanical limits follow ASTM A928/A928M and S32750 grade requirements; all delivered values are verified against the EN 10204 certificate.
Contact Person: Candy
Tel: 008613967883024
Fax: 0086-574-88017980