Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | CHINA |
| Brand Name: | YUHONG |
| Certification: | ABS, GL, DNV, NK, PED, AD2000, GOST9941-81, CCS, ISO 9001-2008 |
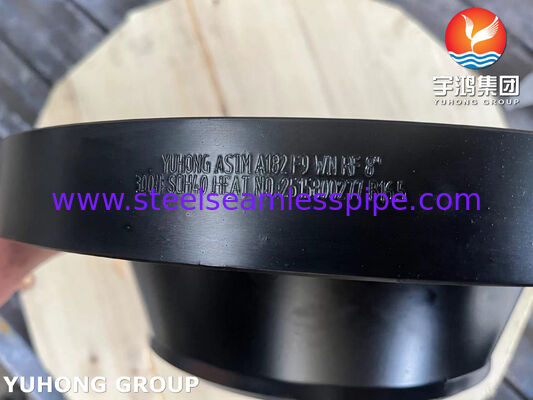
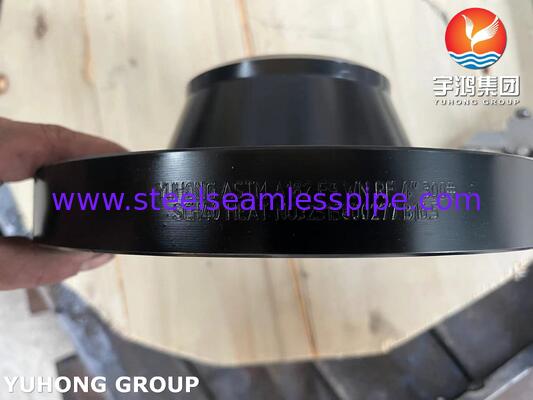
| Model Number: | ASTM A182 F9 Alloy Steel WNRF Flange |
| Minimum Order Quantity: | 1PC |
|---|---|
| Packaging Details: | Plywood Case /Pallet |
| Delivery Time: | 7 DAYS |
| Payment Terms: | L/C,T/T |
| Dimensions: | ANSI Flange, ASME Flange, BS Flange, DIN Flanges, EN Flange | Standard: | B16.5, B16.47 Series A, Series B |
|---|---|---|---|
| Material: | Stainless Steel, Carbon Steel, Alloy Steel, Nickel Alloy | Size: | 1/2" To 48" |
| Thickness: | Sch5S To Sch.XXS | Class: | 150#, 300#, 400#, 600#, 900#, 1500#, 2500# |
| Type: | Welding Neck,Slip-On,Blind, Threaded,Socket Weld,Lap Joint,Orifice Flange | Surface: | FF,RF, RTJ |
| Packaging: | Plywood Case /Pallet | ||
| Highlight: | ASTM A182 F9 weld neck flange,ASME B16.5 forged WNRF flange,alloy steel flange high temperature |
||
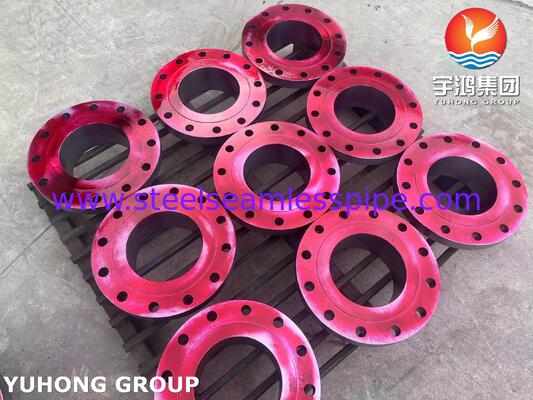
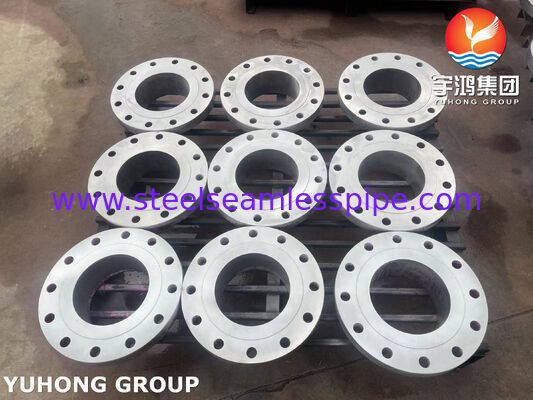
ANSI / ASME B16.5 Forged Flange ASTM A182 F9 Alloy Steel Flange Weld Neck / WNRF Flange
This product is a forged weld neck flange, raised face (WNRF), manufactured from ASTM A182 Grade F9 alloy steel — a 9% chromium, 1% molybdenum ferritic steel supplied in the normalized-and-tempered condition. Dimensional and pressure–temperature requirements follow ASME B16.5, material requirements follow ASTM A182/A182M, and the flange is joined to pipe by a full-penetration butt weld through its tapered hub.
The part exists to solve one specific problem: sealing a bolted joint at temperatures where carbon steel stops being predictable. Above roughly 425 °C, carbon steel loses creep strength and starts to graphitize; the joint relaxes, bolt load drops, and the gasket leaks. Grade F9 keeps useful creep rupture strength up to about 650 °C, resists oxidation far better than 1.25Cr or 2.25Cr grades, and still machines and welds with conventional 9Cr procedures — without the cost premium and the tight PWHT window of Gr 91.
What separates a good F9 flange from an average one is not the drawing, it is the process control behind it: chemistry within the 8.00–10.00% Cr and 0.90–1.10% Mo window, correct normalizing and tempering rather than a shortcut anneal, hardness checked on every piece, 100% positive material identification, and a hub-to-wall transition that is machined, not blended by hand. Those are the details that decide whether the flange survives 200 thermal cycles or fails at the weld toe in the third year.
Equivalent Grades of ASTM A182 Grade F9 Alloy Steel Weld Neck Flanges
| STANDARD | UNS | DIN WERKSTOFF NR. | DIN |
| Alloy F9 | K90941 | 1.7386 | X 12 CrMo 9 1 |
Chemical Composition % of ASTM A182 Grade F9 Alloy Steel Weld Neck Flanges
| Grade | C | Mn | Si | S | P | Cr | Mo |
| A182 F9 | 0.15 | 0.3-0.6 | 0.5-1 | 0.03 | 0.03 | 8-10 | 0.9-1.1 |
Mechanical Properties of ASTM A182 Grade F9 Alloy Steel Weld Neck Flanges
| Grade | Tensile Strength (Mpa) | Yield Strength (Mpa) | Elongation % |
| A182 F9 | 380 | 585 | 20 |
Product scope by flange standard
| Standard | Scope covered in production |
|---|---|
| ANSI B16.5 / ASME B16.47 | 1/2" to 80" (DN15-DN2000); welding neck, slip on, blind, socket weld, threaded and lap joint designs; 150#, 300#, 600#, 900#, 1500#, 2500#; weld neck wall thickness STD, SCH40, SCH80, SCH160, SCHXXS; coatings black paint, yellow transparent paint, cold and hot dip galvanizing |
| EN 1092-1 | DN15-DN2000; type 01 plate, type 02 loose, type 05 blind, type 11 welding neck, type 12 slip on, type 13 threaded; PN6, PN10, PN16, PN25, PN40, PN64, PN100; carbon steel C22.8, S235, S235JR, P235GH and stainless 304/304L, 316/316L |
| DIN | DN15-DN2000; slip on DIN 2573, 2576, 2502, 2503, 2543, 2545; welding neck DIN 2631-2635; blind DIN 2527 PN6-PN40; threaded DIN 2565-2567; loose DIN 2641, 2642, 2656, 2673; carbon steel ST37.2 and stainless 1.4301, 1.4404 |
F9 weld neck flanges are produced to the ASME B16.5 row of the table above; the EN and DIN rows describe the wider flange programme available from the same forging line.
Manufacturing and Quality Control
Forging — billet cut, heated and forged to shape so the grain flow follows the hub-to-flange transition; no welded-in hub, no cast repair.
Heat treatment — full normalize followed by tempering in a calibrated furnace, with the charge chart retained and attached to the MTC.
Machining — face, raised face and bore machined in one set-up where size permits, so face-to-bore squareness stays inside B16.5 tolerances.
Inspection — PT, PMI, dimensional check against class-specific B16.5 tables, face finish verified with a comparator.
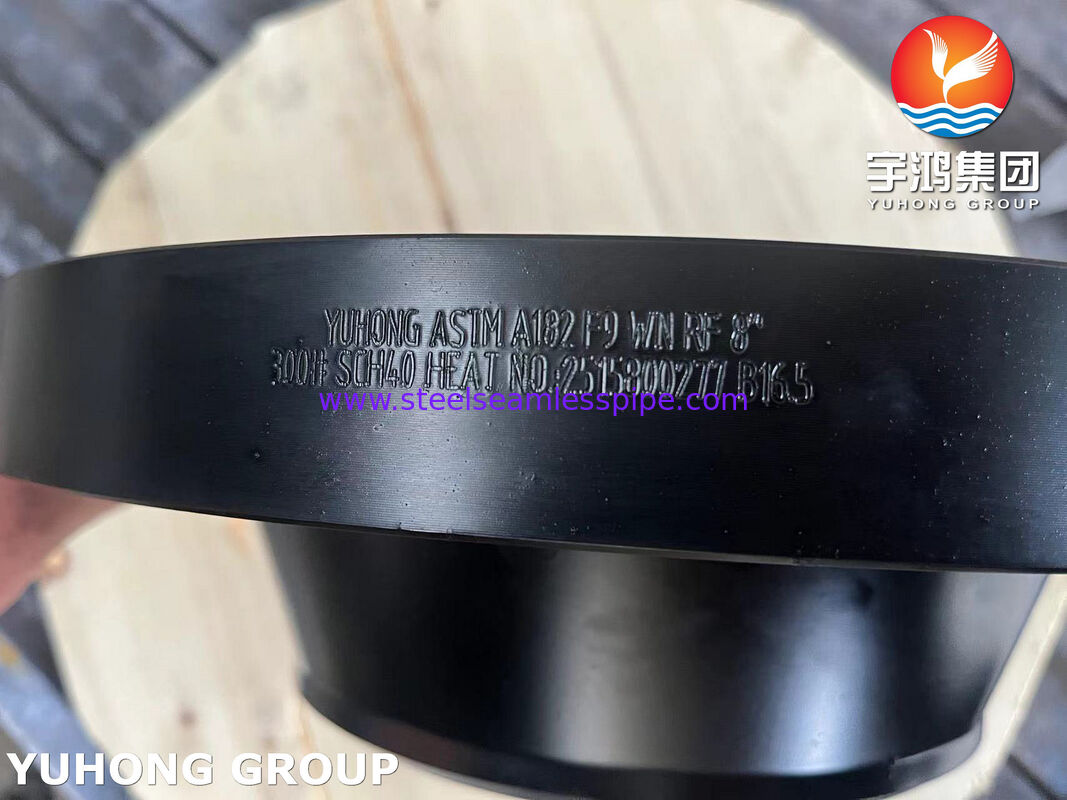
Marking and packing — grade, class, size, heat number and manufacturer mark stamped per B16.5; faces protected, pieces crated for sea freight.
Applications
F9 weld neck flanges are normally found at the hot end of a plant - the positions where the line temperature rules out carbon steel and the fluid rules out austenitic stainless:

Contact Person: Vivi
Tel: 0086-13023766106
Fax: 0086-574-88017980