Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | China |
| Brand Name: | YUHONG |
| Certification: | ISO9001:2015; ISO14001:2015; ISO45001:2018; PED 2014/68/EU; WPS/PQR/WPQ; ISO 3834 |
| Model Number: | N/A |
| Minimum Order Quantity: | 500kgs |
|---|---|
| Price: | To be discussed |
| Packaging Details: | Iron frame wooden case |
| Delivery Time: | 50-120 days |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 5000 meters/day |
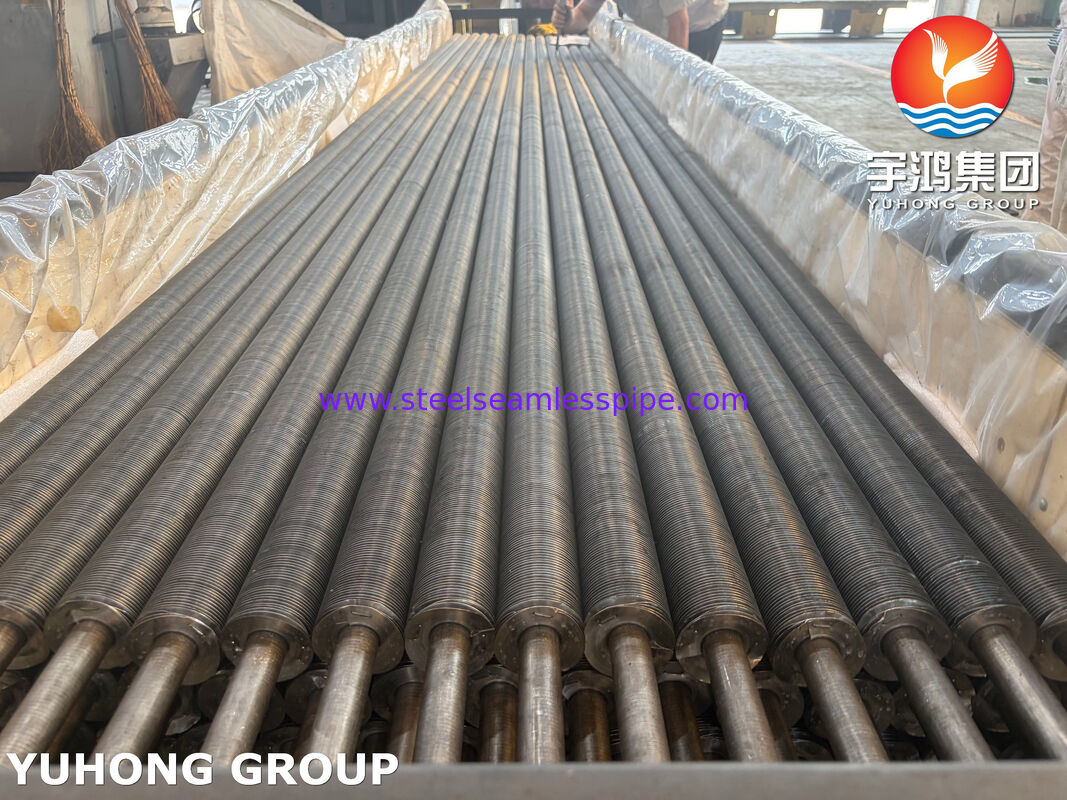
| Product: | Wounded Fin Tube | Material: | ASTM A179 A179 |
|---|---|---|---|
| Application: | Air Coolers | Package: | Iron Frame Wooden Case |
Wound Fin Tube for Air Coolers — ASTM A179
Product Overview
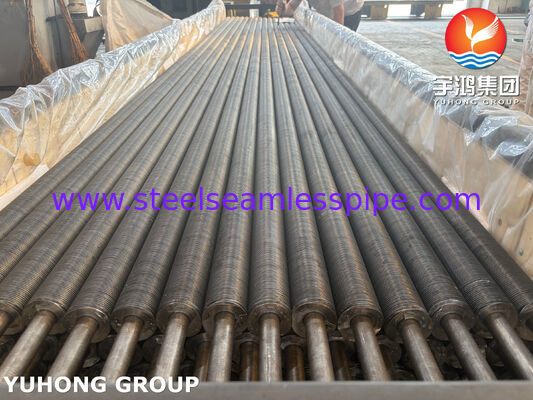
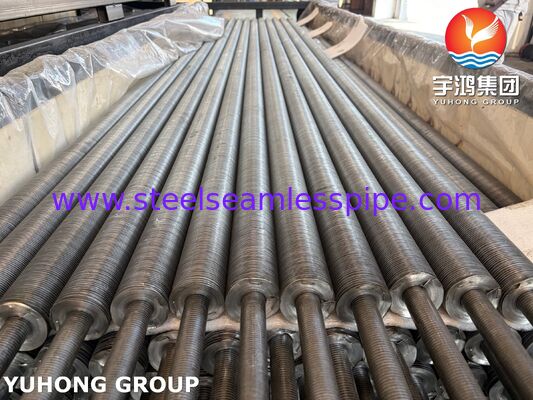
Our wound fin tubes for air coolers, manufactured with ASTM A179 seamless low-carbon steel tubes, are designed to provide efficient air-side heat transfer in air-cooled heat exchangers (ACHE), air-cooled condensers, process air coolers, and other industrial cooling equipment.
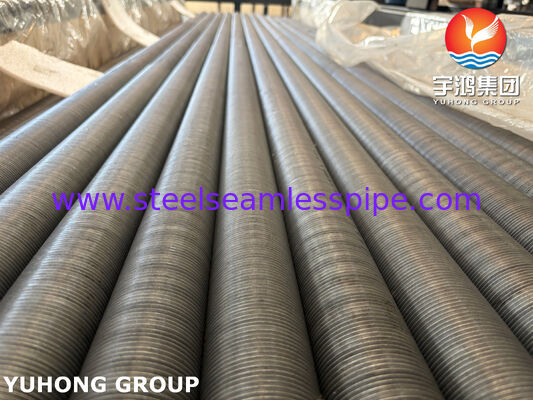
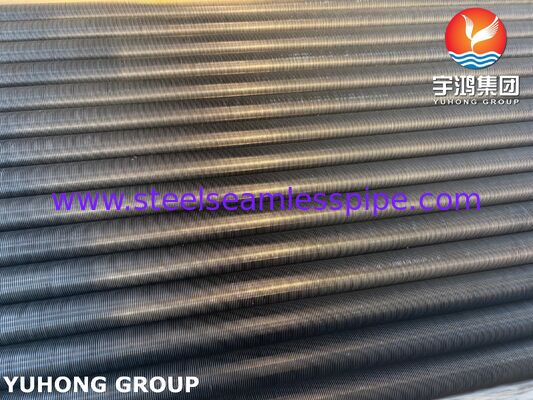
The fin strip is helically wound around the outside surface of the base tube to increase the external heat-transfer area while maintaining a compact tube arrangement. The wound-fin construction provides a practical balance between heat-transfer performance, mechanical strength, manufacturing flexibility, and cost.
ASTM A179 is widely selected for the base tube where good thermal conductivity, weldability, and reliable mechanical performance are required in non-corrosive or moderately corrosive heat-transfer services.
The following dimensions represent commonly manufactured ranges rather than limitations. Final dimensions should be selected according to the thermal design and project specification.
| Item | Typical Range |
|---|---|
| Base tube OD | 16–63.5 mm |
| Base tube wall thickness | 1.5–6.0 mm |
| Tube length | Up to approximately 18 m, subject to transportation and equipment requirements |
| Fin height | 5–25 mm |
| Fin thickness | 0.3–1.2 mm |
| Fin pitch | 2.0–12 mm |
| Fin material | Carbon steel, aluminum, stainless steel or specified alloy |
| Fin type | Helically wound / wrapped |
| Fin coverage | Continuous or specified spacing |
Common base-tube sizes can be supplied according to customer drawings, heat-transfer calculations, or applicable project standards.
ASTM A179 specifies a low-carbon seamless heat-exchanger and boiler tube material. Typical chemical requirements include:
| Element | ASTM A179 Requirement |
|---|---|
| Carbon (C) | ≤ 0.06% |
| Manganese (Mn) | 0.27–0.63% |
| Phosphorus (P) | ≤ 0.035% |
| Sulfur (S) | ≤ 0.035% |
The chemical composition of the supplied material is verified against the applicable material certificate and purchase specification.
Typical minimum mechanical requirements include:
| Property | Requirement |
|---|---|
| Tensile strength | ≥ 325 MPa |
| Yield strength | ≥ 180 MPa |
| Elongation | ≥ 35% |
Actual supplied material shall comply with the applicable edition of ASTM A179/ASME SA179 and the customer's purchase requirements.
Quality control can include:
Additional NDT, PMI, coating inspection, or customer-specific testing can be arranged when required.
ASTM A179 wound fin tubes are commonly used in:
For air coolers, the air side generally represents the greater heat-transfer resistance because air has a much lower heat-transfer coefficient than many process fluids. Increasing the external surface area with fins allows a larger heat-transfer duty to be achieved within a practical equipment footprint.
The wound-fin configuration provides a continuous helical fin surface around the tube and can be manufactured with different fin heights, pitches, and materials to meet different thermal-design requirements.
We can manufacture ASTM A179 wound fin tubes according to:
Contact Person: Nacy
Tel: +8619965117039
Fax: 0086-574-88017980