Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | CHINA |
| Brand Name: | YUHONG |
| Certification: | ISO9001:2015; ISO14001:2015; ISO45001:2018; PED 2014/68/EU; |
| Model Number: | HFW FIN TUBE |
| Minimum Order Quantity: | 10 pc |
|---|---|
| Price: | Negotiable |
| Packaging Details: | IRON FRAME WOODEN CASE |
| Delivery Time: | Negotiable |
| Payment Terms: | T/T,L/C |
| Supply Ability: | 1000 tons per month |
| Base Tube Material: | TP321H (ASME SA312 / ASTM A312) Stainless Steel | Fin Material: | Carbon Steel (CS) |
|---|---|---|---|
| Manufacturing Process: | High Frequency Welding (HFW) / High Frequency Resistance Welding | Application: | Heat Exchanger, Boiler Economizer, HRSG, Waste Heat Recovery, Fired Heater, Air Preheater |
| Industry: | Power Generation, Petrochemical, Refining, Metallurgy | Max Operating Temperature: | Up To 650–750°C (depending On Conditions) |
| Key Advantage: | High Heat Transfer Efficiency + Cost-Effective CS Fins + Excellent High-Temperature Strength Of TP321H |
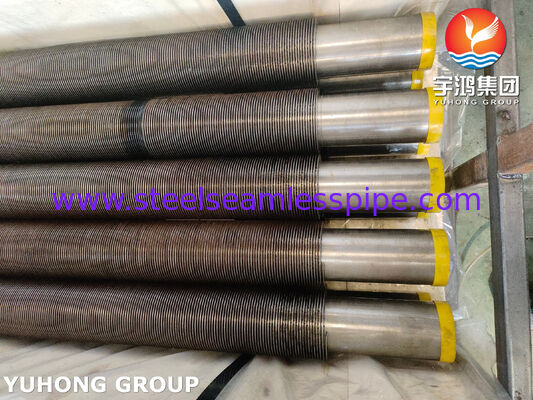
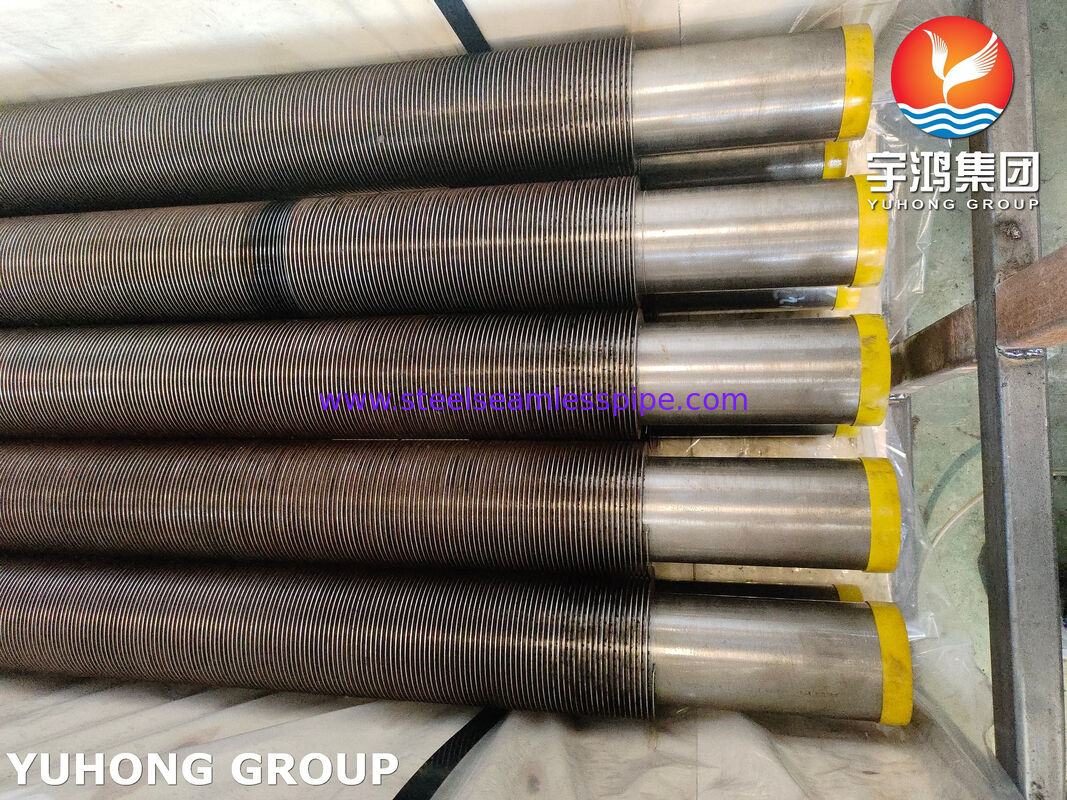
TP321H High Frequency Welded Finned Tube with Carbon Steel (CS) Fins for Waste Heat Recovery Systems
In high-temperature waste heat recovery units (WHRU), HRSG economizers, and process heater convection sections, operators face rapid efficiency loss from limited surface area, thermal fatigue, and material degradation under cyclic flue gas exposure (typically 400–750 °C). Our TP321H base tube + CS fin high-frequency welded (HFW) finned tubes deliver metallurgical bonding that multiplies external heat transfer area while maintaining tube-side integrity against creep and intergranular attack. This combination recovers more energy from exhaust streams, reduces fuel consumption, and extends equipment run time between outages.
The tube consists of a seamless or welded TP321H (UNS S32109) austenitic stainless steel base tube with continuous helical carbon steel fins attached by high-frequency resistance welding. The fin strip is edge-wound under controlled tension while a high-frequency current (typically 200–450 kHz) generates localized resistance heat at the fin root–tube interface. Applied forge pressure creates a continuous metallurgical bond without filler metal. Weld penetration and bond strength are verified by peel tests and metallographic examination, achieving fin-to-tube contact efficiency ≥95 % and eliminating air-gap thermal resistance.
TP321H Base Tube (ASTM A312 / ASME SA312)
| Element | Composition (%) |
|---|---|
| Carbon (C) | 0.04 – 0.10 |
| Manganese (Mn) | ≤ 2.00 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.030 |
| Silicon (Si) | ≤ 1.00 |
| Chromium (Cr) | 17.0 – 19.0 |
| Nickel (Ni) | 9.0 – 12.0 |
| Titanium (Ti) | 4×(C+N) min – 0.70 max |
| Nitrogen (N) | ≤ 0.10 |
| Iron (Fe) | Balance |
Carbon Steel Fins (typical low-carbon grades such as Q235 / SPCC / equivalent)
| Element | Typical Composition (%) |
|---|---|
| Carbon (C) | 0.12 – 0.20 |
| Manganese (Mn) | 0.30 – 0.70 |
| Phosphorus (P) | ≤ 0.045 |
| Sulfur (S) | ≤ 0.045 |
| Silicon (Si) | ≤ 0.30 |
| Iron (Fe) | Balance |
| Parameter | Standard Range | Typical Tolerance |
|---|---|---|
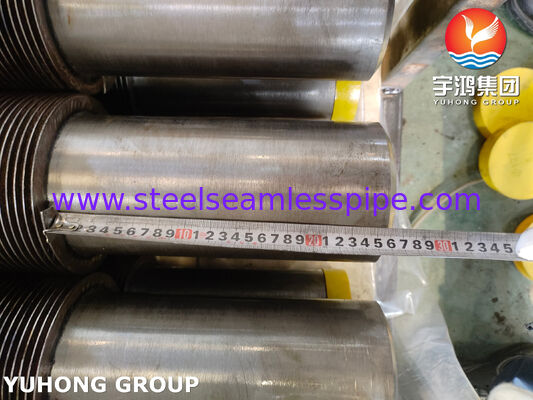
| Base Tube OD | 15 – 219 mm | ±0.25 mm or ±0.5 % |
| Base Tube Wall Thickness | 1.0 – 12 mm | ±10 % of nominal |
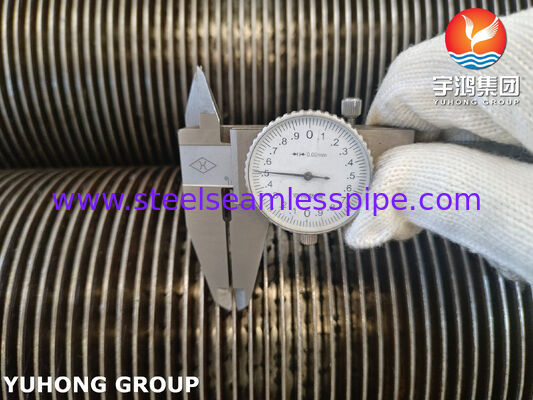
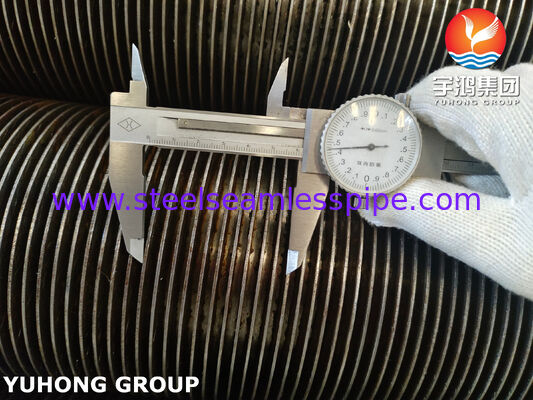
| Fin Height | 8 – 30 mm | ±0.5 mm / ±1.0 mm |
| Fin Thickness | 0.8 – 3.0 mm | ±0.1 mm |
| Fin Pitch / Density | 3 – 25 mm (1–8 FPI) | ±5 % over 300 mm length |
| Tube Length | Up to 18–24 m (custom) | ±5–10 mm |
| Unfinned Ends | 50 – 300 mm (as required) | — |
Custom dimensions outside the above ranges are available upon engineering review.
These TP321H/CS HFW finned tubes are engineered for continuous duty in:
In these services the product directly addresses efficiency shortfalls caused by insufficient surface area and material limitations of plain tubes or lower-grade finned tubes, delivering measurable gains in recovered heat and reduced auxiliary fuel use.
Tubes are packed in seaworthy plywood cases or steel-frame wooden crates with internal supports to prevent fin deformation. Tube ends are capped with plastic protectors; external surfaces receive temporary anti-rust oil or VCI protection as required. Marking includes heat number, size, material grade, and order reference. Standard export packing supports FCL/LCL shipment; special length or project packaging can be arranged.
All material is supplied with EN 10204 3.1 Mill Test Certificates covering chemical analysis, mechanical properties, and heat treatment. Production inspections include dimensional verification, weld integrity (peel / visual / NDT as specified), hydrostatic or pneumatic testing of the base tube, and final visual examination. Optional third-party inspection (SGS, BV, Lloyd’s, etc.) is available.
Commercial Terms
Contact us with your design parameters (tube OD, wall thickness, fin height/pitch, length, quantity, and design temperature/pressure) for a project-specific quotation and detailed technical data sheet.
Contact Person: Freya
Tel: +8617276485535
Fax: 0086-574-88017980