Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | China |
| Brand Name: | YUHONG |
| Certification: | ISO9001:2015; ISO14001:2015; ISO45001:2018; PED 2014/68/EU; WPS/PQR/WPQ; ISO 3834 |
| Model Number: | N/A |
| Minimum Order Quantity: | 500kgs |
|---|---|
| Price: | To be discussed |
| Packaging Details: | Plywood case or Iron frame wooden case |
| Delivery Time: | 50-120 days |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 5000 meters/day |
| Product: | Studded Fin Tube | Material: | ASTM A335 P22 |
|---|---|---|---|
| Application: | Waste Heat Recovery | Package: | Plywood Case Or Iron Frame Wooden Case |
| Highlight: | ASTM A335 P22 studded tubes,waste heat recovery fin tubes,studded tubes for heat recovery |
||
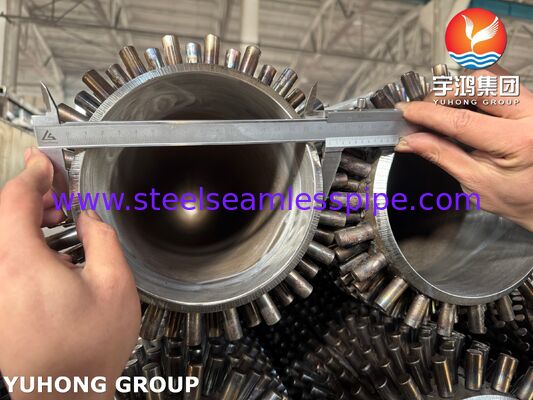
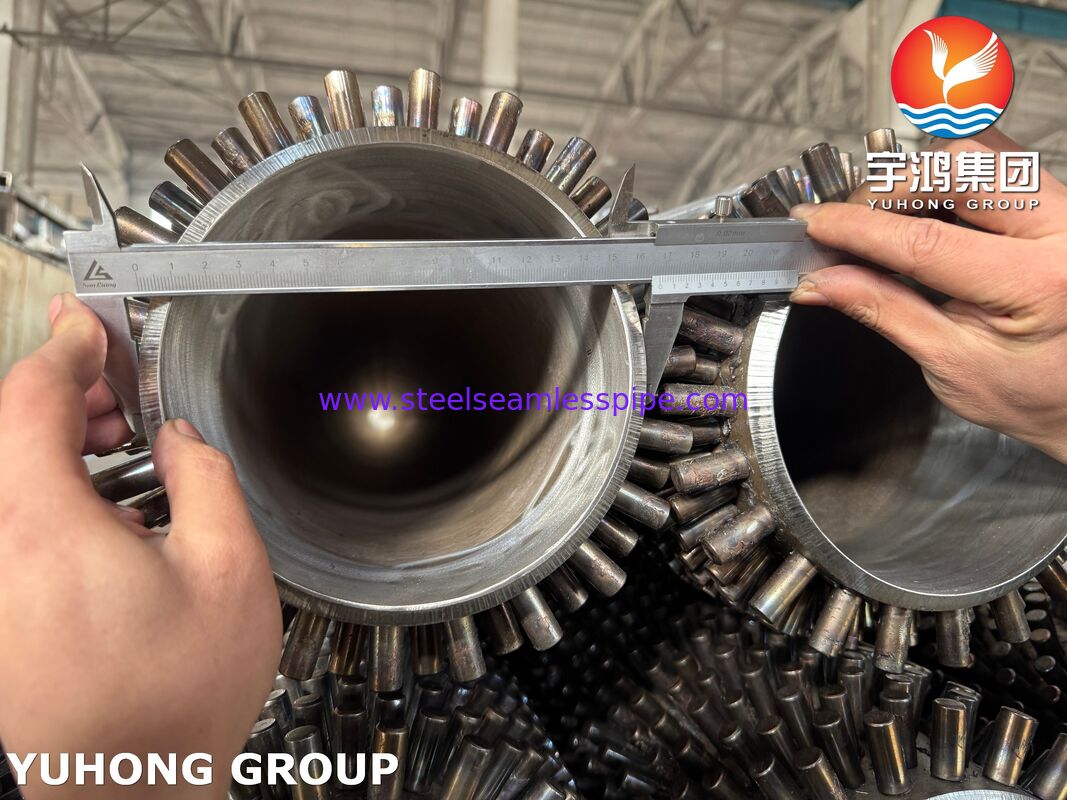
ASTM A335 P22 Studded Tubes for Waste Heat Recovery are high-temperature heat-transfer tubes designed for recovering thermal energy from hot flue gas, exhaust gas, and other high-temperature process streams.
The tubes use ASTM A335 P22 seamless alloy steel as the base tube. P22 is a chromium-molybdenum alloy steel containing approximately 2.25% chromium and 1% molybdenum, providing a combination of elevated-temperature strength, oxidation resistance, and thermal stability. The external surface is fitted with individually welded studs that increase the effective gas-side heat-transfer area.
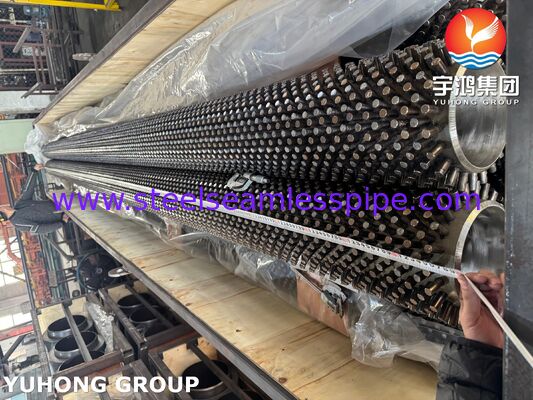
Unlike conventional continuous finned tubes, studded tubes use discrete cylindrical or specially shaped studs arranged around the tube. This configuration provides additional heat-transfer surface while maintaining open gas-flow passages, making the design particularly useful for fouling, dusty, erosive, and high-temperature waste-gas applications.
Our ASTM A335 P22 studded tubes can be manufactured according to customer drawings, thermal-design requirements, applicable codes, and project specifications.
The exact dimensions of a studded tube should be determined by the thermal calculation and mechanical design of the waste heat recovery equipment.
| Item | Typical Range / Specification |
|---|---|
| Base Tube Material | ASTM A335 P22 |
| Base Tube Type | Seamless alloy steel tube |
| Outside Diameter | Approx. 25.4–114.3 mm |
| Wall Thickness | Approx. 3.0–12.5 mm |
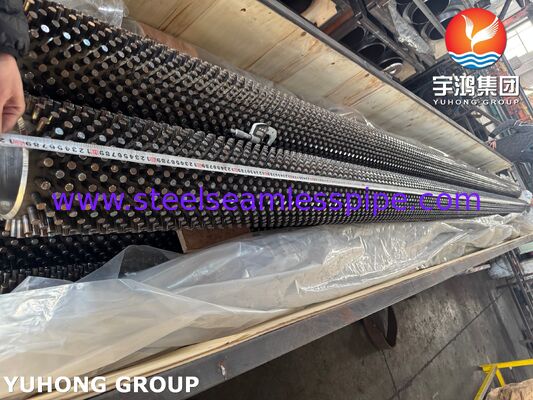
| Tube Length | Approx. 3,000–18,000 mm |
| Stud Material | Carbon steel, alloy steel, or specified material |
| Stud Height | Approx. 12.7–63.5 mm |
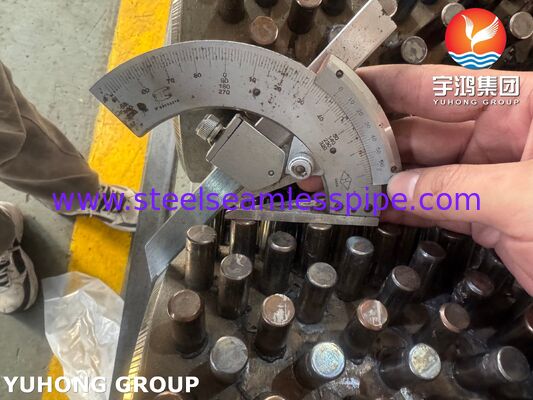
| Stud Diameter | Approx. 6–25 mm |
| Stud Pitch | Approx. 15–50 mm, or according to design |
| Stud Pattern | In-line / staggered / customized |
| Stud Attachment | Resistance welding or qualified welding process |
| Heat Treatment | According to ASTM A335 and project requirements |
| Surface Condition | As manufactured, shot blasted, coated, or specified |
| Certification | EN 10204 3.1 / project-specific documentation available |
The above ranges are typical manufacturing ranges rather than fixed ASTM dimensional requirements. Final dimensions are normally established by the customer's thermal design, drawings, pressure calculations, and applicable fabrication standards.
The ASTM A335 P22 base tube is a 2¼Cr-1Mo alloy steel. The principal alloying elements provide improved high-temperature performance compared with conventional carbon-steel tubes.
| Element | Chemical Composition, wt.% |
|---|---|
| Carbon (C) | 0.05–0.15 |
| Manganese (Mn) | 0.30–0.60 |
| Silicon (Si) | ≤ 0.50 |
| Phosphorus (P) | ≤ 0.025 |
| Sulfur (S) | ≤ 0.025 |
| Chromium (Cr) | 1.90–2.60 |
| Molybdenum (Mo) | 0.87–1.13 |
Chromium (Cr) contributes to oxidation resistance and high-temperature stability.
Molybdenum (Mo) improves elevated-temperature strength and resistance to softening during prolonged service.
The Cr-Mo alloy system makes P22 suitable for heat-recovery equipment operating at temperatures where ordinary carbon-steel tubing may have insufficient long-term performance.
Typical minimum mechanical requirements for ASTM A335 P22 include:
| Property | Requirement |
|---|---|
| Tensile Strength | ≥ 415 MPa |
| Yield Strength | ≥ 205 MPa |
| Elongation | ≥ 30%* |
| Heat Treatment | Normalized and tempered, as specified |
| Hardness | According to applicable ASTM A335 requirements |
Elongation requirements can depend on tube dimensions and the applicable specification provisions. Final inspection is performed according to the ordered ASTM/ASME specification.
The mechanical properties of P22 allow the base tube to withstand the combination of internal pressure, elevated temperature, thermal cycling, and mechanical loading encountered in waste heat recovery equipment.
The studded configuration is designed to increase the external heat-transfer surface without creating a continuous fin wall.
Individual studs are distributed around the tube circumference and along the tube length. When hot gas passes across the studded surface, the additional surfaces promote gas-side heat transfer.
The design can be optimized by adjusting:
For dusty or fouling gas streams, the spacing between studs can also be considered during thermal and pressure-drop calculations.
Our ASTM A335 P22 studded tubes can be produced through a controlled manufacturing sequence:
ASTM A335 P22 seamless tubes are inspected for dimensional accuracy, surface condition, material identification, and traceability.
The tube surface is cleaned and prepared to provide suitable conditions for stud attachment.
Studs are manufactured to the specified diameter, height, geometry, and material requirements.
The studs are attached to the tube using a controlled welding process selected according to the tube material, stud material, design, and project specification.
Where required by the material specification, welding procedure, engineering design, or customer specification, suitable post-weld heat treatment or stress-relief procedures can be applied.
The finished tubes are checked for tube dimensions, stud dimensions, pitch, alignment, straightness, and overall workmanship.
Inspection records, material certificates, dimensional reports, and applicable NDT reports can be supplied according to the agreed inspection plan.
Quality control is especially important for studded tubes because both the pressure-retaining base tube and the stud attachment affect service performance.
Chemical analysis is performed to verify that the base tube complies with ASTM A335 P22 chemistry.
Tensile testing verifies tensile strength, yield strength, and elongation.
Hardness testing can be performed to verify compliance with the applicable material and heat-treatment requirements.
Hydrostatic testing can be performed on the base tube according to ASTM A335 and the customer's inspection requirements.
Eddy current examination may be used to detect certain surface and near-surface discontinuities in the tube.
Ultrasonic testing can be provided where required by the purchase specification, quality plan, or applicable code.
Visual inspection covers:
Typical dimensional checks include:
Representative stud joints can be subjected to attachment-strength or weld-quality testing according to the agreed manufacturing procedure and customer specification.
Heat numbers and material identification can be maintained from the raw P22 tube through manufacturing and final inspection. EN 10204 3.1 material certificates can be supplied when specified.
P22 provides better elevated-temperature mechanical performance than conventional carbon-steel tubing for demanding heat-recovery service.
The studs increase the external heat-transfer surface, allowing more thermal energy to be transferred from hot gas to the fluid inside the tube.
The open stud arrangement can provide gas-flow passages between individual heat-transfer elements, which can be advantageous where ash, dust, or other deposits are present.
Individual welded studs provide a mechanically robust heat-transfer surface suitable for industrial equipment exposed to vibration and thermal cycling.
Stud height, diameter, density, and arrangement can be adjusted to balance heat-transfer requirements, gas-side pressure drop, fouling characteristics, and equipment dimensions.
ASTM A335 P22 studded tubes can be used in waste heat recovery boilers to recover thermal energy from high-temperature exhaust gases.
Suitable for recovering energy from exhaust streams generated by industrial furnaces, process equipment, and high-temperature production systems.
P22 studded tubes can be considered for selected high-temperature convection and waste-heat recovery sections in refinery and petrochemical facilities.
The studded configuration can be used in high-temperature convection sections where increased heat-transfer surface and resistance to demanding gas-side conditions are required.
Applications may include selected boiler and heat-recovery surfaces in thermal power and combined-cycle power facilities.
P22 studded tubes can be engineered for selected high-temperature heat-recovery sections associated with gas-turbine exhaust systems, subject to the specific thermal and mechanical design.
They can be considered for heat recovery from hot combustion gases where the equipment design requires a durable enhanced heat-transfer surface.
We manufacture studded tubes according to the customer's tube dimensions, stud geometry, thermal requirements, material specification, and inspection plan.
Our production and inspection approach focuses on:
Whether required for a waste heat recovery boiler, fired heater, industrial furnace, refinery unit, or power-generation heat recovery system, ASTM A335 P22 studded tubes can be engineered as a durable high-temperature heat-transfer solution.
Product: Studded Tubes for Waste Heat Recovery
Base Tube: ASTM A335 P22
Material: 2¼Cr-1Mo Alloy Steel
Tube Type: Seamless
Stud Type: Cylindrical / rectangular / customized
Stud Arrangement: In-line / staggered / customized
Application: Waste Heat Recovery
Temperature Service: High-temperature service, according to engineering design
Testing: Chemical analysis, tensile, hardness, hydrostatic, NDT, dimensional and visual inspection as applicable
Documentation: MTC / EN 10204 3.1 / inspection reports available upon request
Customization: Available according to drawings and thermal-design requirements
Contact Person: Nacy
Tel: +8619965117039
Fax: 0086-574-88017980