Yuhong Holding Group Co.,LTD
 |
| Place of Origin: | China |
| Brand Name: | YUHONG |
| Certification: | ISO9001:2015; ISO14001:2015; ISO45001:2018; PED 2014/68/EU; WPS/PQR/WPQ; ISO 3834 |
| Model Number: | N/A |
| Minimum Order Quantity: | 500kgs |
|---|---|
| Price: | To be discussed |
| Packaging Details: | Plywood case or Iron frame wooden case |
| Delivery Time: | 50-120 days |
| Payment Terms: | L/C,T/T |
| Supply Ability: | 5000 meters/day |
| Product: | HFW Fin Tube | Material: | ASTM A192 A192 |
|---|---|---|---|
| Application: | Superheater | Package: | Plywood Case Or Iron Frame Wooden Case |
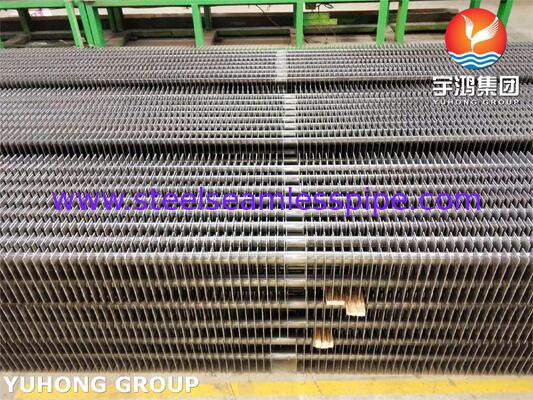
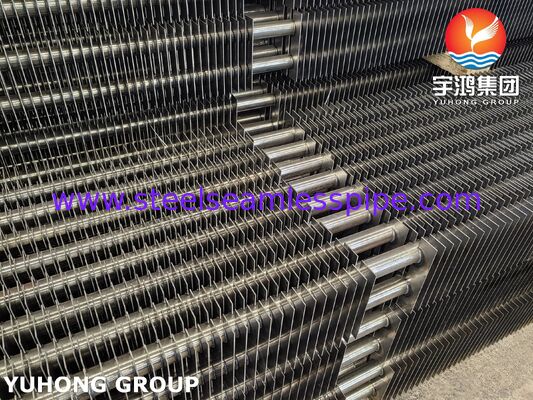
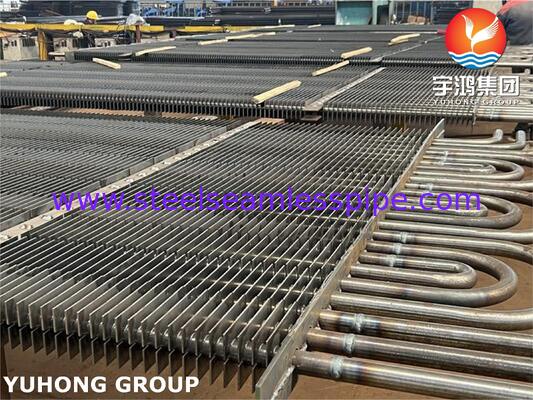
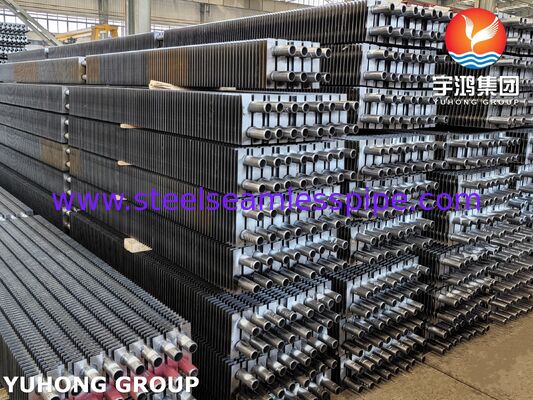
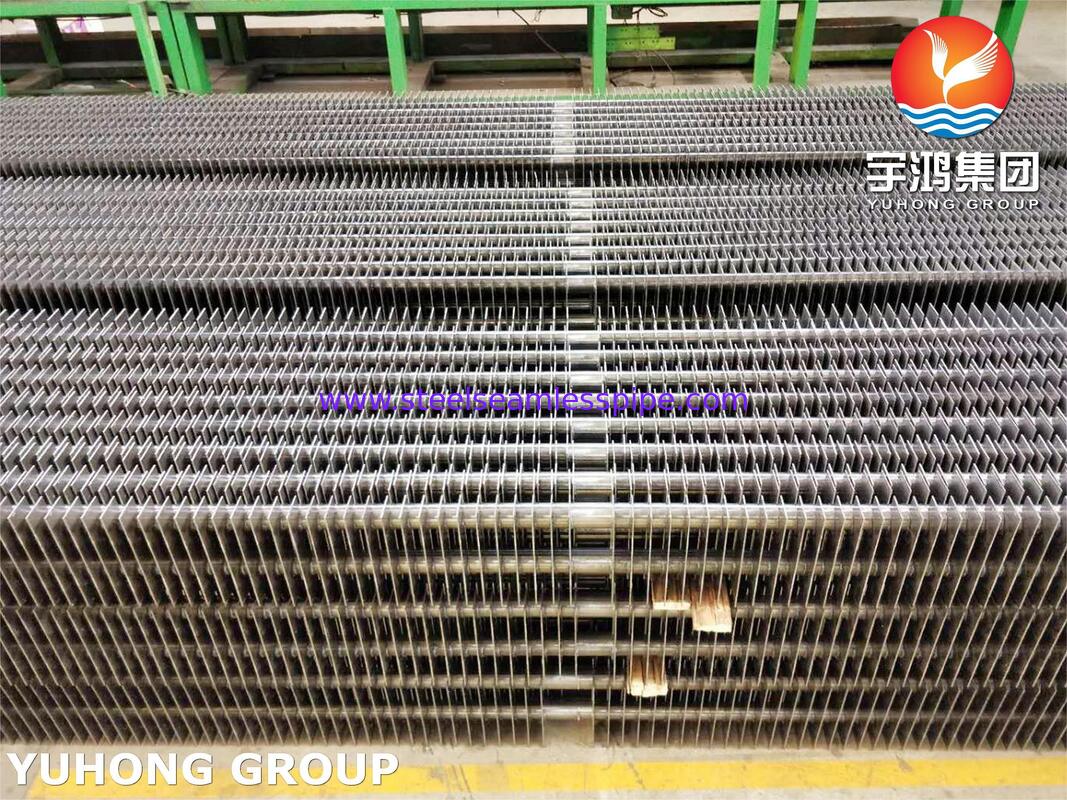
High-frequency welded finned tubes for superheaters are engineered heat-transfer components designed to improve thermal efficiency in industrial boilers, power plants, waste-heat recovery units, and steam-generation systems. Manufactured with an ASTM A192 carbon steel base tube and high-frequency welded fins, these products increase the effective heat-transfer surface area, helping equipment recover more heat from hot flue gas and transfer it to boiler water or steam.
Our high-frequency welded finned tubes combine a pressure-bearing carbon steel tube with firmly attached fins to provide efficient heat exchange, reliable construction, and flexible configuration options for demanding thermal applications. Tube dimensions, fin geometry, and material specifications can be customized to meet project requirements and equipment design conditions.
Important material note: ASTM A192/A192M covers seamless carbon steel boiler and superheater tubes for high-pressure service. The standard does not itself define the complete high-frequency fin-welding process, so the finished finned-tube assembly should be specified with separate requirements for fin material, weld integrity, dimensional tolerances, and inspection.
Key Product FeaturesEnhanced heat-transfer performance: Fins expand the external heat-transfer area, supporting more effective heat recovery from flue gas.
High-frequency welded fin attachment: The welding process creates a continuous, secure connection between the fin strip and base tube when manufactured to qualified procedures.
Carbon steel pressure tube: ASTM A192 material is suitable for specified boiler and superheater service conditions when design limits are respected.
Customizable fin geometry: Fin height, thickness, pitch, and configuration can be selected to balance heat-transfer performance, gas-side pressure drop, and resistance to fouling.
Flexible manufacturing options: Tube length, fin coverage, end preparation, and un-finned sections can be tailored to the boiler layout.
Quality-focused production: Material traceability, dimensional inspection, and appropriate weld-integrity testing help support consistent manufacturing quality.
Industrial boiler superheaters
Used in suitable boiler configurations to improve gas-side heat transfer and support steam-temperature control.
Power generation
Applied in boiler heat-recovery sections where the operating temperature, pressure, and corrosion environment are compatible with the selected carbon steel.
Waste-heat recovery systems
Helps recover useful thermal energy from industrial exhaust gases in appropriately designed heat-recovery equipment.
Standard Size RangesThe following are typical commercial manufacturing ranges for high-frequency welded finned tubes. They are indicative, not dimensional requirements mandated by ASTM A192. Final dimensions should be agreed upon according to the boiler design, heat-transfer calculations, and project specifications.
Parameter |
Typical range |
|---|---|
Base tube outside diameter |
19.05–76.2 mm |
Base tube wall thickness |
2.0–8.0 mm |
Tube length |
3,000–18,000 mm |
Fin height |
10–25 mm |
Fin thickness |
0.8–1.5 mm |
Fin pitch |
2.5–8.0 mm |
Fin material |
Carbon steel or another specified compatible material |
Fin configuration |
Solid, serrated, or project-specific profile |
Fin attachment |
High-frequency resistance welding |
Customization: Other dimensions may be available subject to manufacturing capability. Please confirm the base tube diameter, wall thickness, fin material, fin pitch, fin height, tube length, and applicable code before ordering.
ASTM A192 Chemical CompositionASTM A192/A192M-24 specifies the following chemical composition limits for the carbon steel tube.
Element |
Composition, wt.% |
|---|---|
Carbon (C) |
0.06–0.18 |
Manganese (Mn) |
0.27–0.63 |
Phosphorus (P) |
≤ 0.035 |
Sulfur (S) |
≤ 0.035 |
Silicon (Si) |
≤ 0.25 |
These limits apply to the ASTM A192 base tube material, not automatically to the fin strip. The fin material must comply with its own specified grade and chemical composition requirements.
Mechanical PropertiesTypical specified mechanical requirements for ASTM A192 carbon steel boiler tubing include the following:
Property |
ASTM A192 requirement |
|---|---|
Tensile strength, minimum |
325 MPa (47 ksi) |
Yield strength, minimum |
180 MPa (26 ksi) |
Elongation in 50.8 mm (2 in.), minimum |
35% |
Brinell hardness, maximum, wall ≥ 5.1 mm |
137 HBW |
Rockwell hardness, maximum, wall < 5.1 mm |
77 HRBW |
Seamless Carbon Steel Boiler Tubes Standard
+1
Mechanical properties are determined for the base tube in accordance with the applicable specification and test conditions. They should not be interpreted as guaranteed properties of the entire welded fin assembly. The fin weld and heat-affected zone require appropriate manufacturing and inspection controls.
Manufacturing ProcessBase tube preparation: Procure and verify seamless ASTM A192 carbon steel tubes, including material identification, dimensions, and traceability.
Surface preparation: Clean the tube and fin contact surfaces to support consistent welding.
Fin forming: Prepare the specified fin strip and control its thickness, height, pitch, and profile.
High-frequency welding: Weld the fin continuously along the tube using a qualified procedure with controlled welding parameters.
Dimensional correction: Check fin alignment, pitch uniformity, tube straightness, and end dimensions.
Finishing: Remove unacceptable weld projections or surface defects using approved methods, without compromising the weld or tube wall.
Final inspection: Verify the finished product against the purchase specification and applicable inspection plan.
A quality assurance plan for high-frequency welded finned tubes for superheaters may include:
Inspection or test |
Purpose |
|---|---|
Material certificate review |
Confirms base tube grade, heat number, and chemical composition |
Chemical analysis |
Verifies compliance with ASTM A192 when required |
Tensile testing |
Checks base tube tensile strength, yield strength, and elongation |
Hardness testing |
Verifies that applicable base tube hardness limits are met |
Dimensional inspection |
Measures tube diameter, wall thickness, fin height, pitch, thickness, and length |
Visual inspection |
Identifies surface defects, irregular fins, and visible weld discontinuities |
Weld-integrity testing |
Evaluates fin-to-tube bond integrity using a qualified method and agreed acceptance criteria |
Hydrostatic testing |
Tests the pressure boundary where required by the applicable tube specification or project |
Nondestructive examination |
Additional methods may be specified based on the weld design, service conditions, and project code |
Final documentation |
Records inspection results, material traceability, and applicable test certificates |
Quality note: ASTM A192 includes requirements for specified tube tests, including flattening, flaring, hardness, and hydrostatic testing, subject to the applicable edition and ordering requirements. The precise inspection and acceptance criteria for the high-frequency fin weld should be defined separately.
Product AdvantagesIncreased effective heat-transfer area compared with a bare tube of the same nominal diameter.
Potential for reduced heat-exchanger size or improved heat recovery, subject to thermal and pressure-drop calculations.
Mechanically attached fins designed for reliable heat transfer when welding quality is properly controlled.
Flexible configuration for new boiler installations and replacement heat-transfer bundles.
Material traceability and inspection documentation available according to the agreed purchase requirements.
Compatibility with selected boiler and superheater applications when the operating temperature, pressure, oxidation, and corrosion conditions are suitable for carbon steel.
To obtain a quotation for high-frequency welded finned tubes for superheaters, please specify:
Base tube standard: ASTM A192/A192M
Base tube outside diameter and wall thickness
Fin material and fin profile
Fin height, thickness, and pitch
Tube length and quantity
Operating temperature and pressure
Applicable ASME or other project code
Required inspection, testing, and documentation
Delivery requirements and packaging
Contact Person: Nacy
Tel: +8619965117039
Fax: 0086-574-88017980